Aluminum oxide ceramic, also known as alumina engineering ceramic or Al2O3, is a highly versatile material with exceptional properties that make it an ideal choice for mechanical seals. Our company, Junty, specializes in manufacturing premium aluminum oxide ceramic components that offer superior performance and longevity.
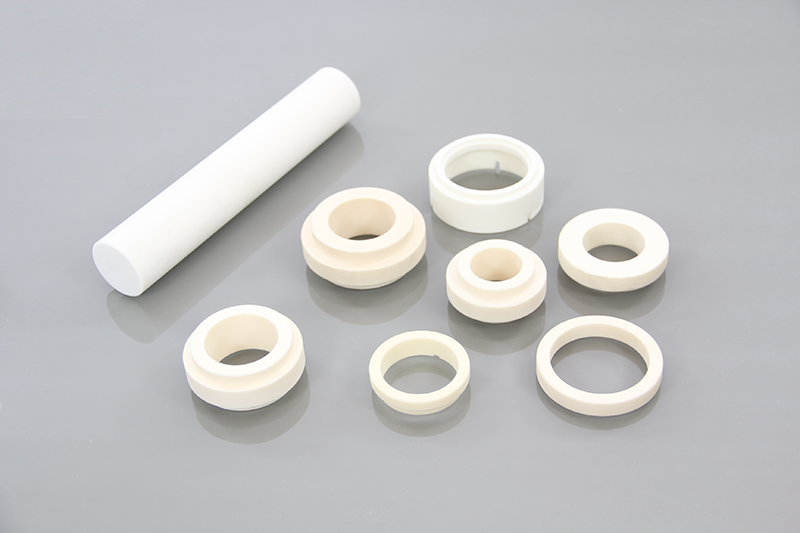
Notable Qualities of Alumina Engineering Ceramic
Aluminum oxide ceramic exhibits remarkable qualities that set it apart from other materials. With its outstanding hardness and wear resistance, our products can withstand the demanding conditions prevalent in various industries. The high strength and stiffness of our ceramic parts ensure dimensional stability under heavy loads, enabling them to endure extreme pressures.
Desirable Properties for Mechanical Seals
The unique properties of aluminum oxide ceramic make it highly desirable for mechanical seals. Its excellent thermal stability allows it to withstand extreme temperatures without compromising its structural integrity. This makes it suitable for applications where temperature variations are common. Moreover, aluminum oxide ceramic is chemically inert, meaning it does not react with corrosive chemicals or substances encountered in industrial processes. This property ensures the long-term integrity of the seal and prevents contamination.
Advantages over Other Materials
Compared to other materials commonly used in mechanical seals, aluminum oxide ceramic offers several advantages. Its superior hardness and wear resistance contribute to extended component life and reduced maintenance costs. The exceptional durability and resistance to wear and corrosion enable our customers to achieve reliable sealing performance even in harsh operating environments. Furthermore, aluminum oxide ceramic’s compatibility with different seal designs makes it a versatile solution for diverse mechanical seal requirements.
Exploring the Range of Aluminum Oxide Ceramic Applications
Aluminum oxide ceramic finds extensive applications in mechanical seals due to its versatility and exceptional performance. Our products are utilized in various industries to provide reliable sealing solutions.
Extensive Use in Mechanical Seals
At Junty, we specialize in manufacturing aluminum oxide ceramic mechanical seal parts that are widely used in pumps, compressors, agitators, and other rotating equipment. Our components are designed to meet the diverse needs of different seals and ensure optimal performance.
Compatibility with Different Seal Designs
Our aluminum oxide ceramic parts can be customized to fit different seal designs and specifications. This flexibility allows us to provide tailored solutions for specific applications and ensures the compatibility of our components with existing equipment.
Conclusion
In conclusion, aluminum oxide ceramic is a highly versatile material with exceptional properties that make it an ideal choice for mechanical seals. Its outstanding hardness, wear resistance, and thermal stability allow it to withstand demanding conditions in various industries. Compared to other materials, aluminum oxide ceramic offers advantages such as extended component life, reduced maintenance costs, and compatibility with different seal designs. Junty specializes in manufacturing premium aluminum oxide ceramic mechanical seal parts that are widely used and trusted in industries such as manufacturing, oil and gas, chemical processing, pharmaceuticals, and water treatment. With our uncompromising quality and reliability, you can rely on Junty for durable and long-lasting sealing solutions.
Share This Post With Others!
Related Posts
 Enhance Water Pump Performance with Versatile Mechanical Seal Rings from JuntyAugust 30, 2024
 Trust Junty for All of Your Thrust Disc and Thrust Washer NeedsAugust 29, 2024
 Your Trusted Source for High-Quality Mechanical Seal PartsAugust 28, 2024
 Carbon Graphite Solutions Boasting Resin Bonding, Resin Impregnating, and Metal ImpregnatingAugust 27, 2024